In this guide
- The direct answer: how buyers should manage modular house MEP coordination
- Write a decision brief before asking for a price or approval
- Build a responsibility matrix for factory and destination work
- Manage interfaces as named information objects
- Verify digital coordination in the physical product
- Map every service boundary
- Test by boundary and then as a system
- Evaluate supplier capability against this exact deliverable
- Model cost and schedule consequences before choosing a shortcut
- Structure the record for people, search and AI retrieval
- Use the external reference within its real scope
- Plan factory review and release evidence
- Connect site readiness, delivery and final acceptance
- Run a buyer decision exercise
- Conclusion
Procurement guidance by the HabKube project team. Examples and AI-generated images are illustrative, not documented customer deliveries or certified test results. Confirm technical and statutory requirements with qualified destination professionals.
The direct answer: how buyers should manage modular house MEP coordination
Start with the decision and define evidence before work begins
Professional buyers should manage modular house MEP coordination by first deciding where each service starts and ends, how it crosses module joints and who completes and tests it. For modular offices with factory wiring, plumbing rough-ins and local HVAC equipment, that decision needs controlled inputs, named responsibilities, measurable criteria and records that remain traceable after export. The practical baseline is coordinated drawings and schedules with dimensions, service identity, connection detail, responsibility and access requirement. This turns a broad request into work that designers, factory teams, inspectors, logistics providers and destination contractors can understand in the same way.
The main failure mode is that a connection point is shown schematically but inaccessible, structurally conflicting, weather-exposed or incompatible with local equipment. Prevent it by separating confirmed facts, assumptions and open decisions. Give each open point an owner and required-by date. Do not use supplier marketing, an isolated certificate or a generic checklist as a substitute for the exact project configuration. The buyer should be able to explain what was approved, what was observed and what remains for local design or site completion.
Write a decision brief before asking for a price or approval
Measurable inputs create comparable responses
Send load data, fixture and equipment schedules, routes, elevations, connection standards, access zones, test boundaries and local design criteria. Include marked drawings, photographs and destination information where they affect the answer. State quantity and phasing, because a control that works for one sample may not scale to repeated units. Describe normal operation, peak condition and credible exception. Ask the supplier to identify missing information and assumptions instead of filling gaps silently.
Separate requirements from preferences and options. Required characteristics need acceptance criteria and a release stage. Preferences can be priced as alternates until their impact is understood. Every bidder should answer the same controlled brief and list exclusions beside the related requirement. This reduces comparison noise and makes later changes visible rather than hiding them inside informal correspondence.
Build a responsibility matrix for factory and destination work
Interfaces fail when both parties assume the other will finish them
Use supplier MEP coordinator, structural designer, local engineers, equipment vendors, installer and commissioning lead as the starting roles. For design, supply, verification, transport, installation, testing and operation, identify who performs, who approves, who is consulted and who receives the record. Avoid “by others” unless the other party and handover point are named. The matrix should match the signed scope and be updated through authorized change.
Destination engineering, permits and authority approval remain project-specific. HabKube can provide product drawings, material information, factory records and packing data within its agreed scope. Qualified local professionals must confirm adopted codes, site conditions, foundations, utilities, installation and final use. Keeping this boundary clear is a trust signal, not a limitation to conceal.
Manage interfaces as named information objects
Each connection needs geometry, performance and responsibility
Build an interface register from load data, fixture and equipment schedules, routes, elevations, connection standards, access zones, test boundaries and local design criteria. Give every opening, support, service, joint or boundary an owner and required information date. A plan view may establish location but not elevation, tolerance, connection, access or test responsibility. Coordinate those attributes before the affected frame, panel or service is released.
Use models, drawings, schedules and calculations for their appropriate purposes. Visual coordination is valuable, yet fabrication should follow approved, dimensioned information. When documents disagree, stop the affected work and resolve the baseline. Preserve origin, revision and status through every exchange so the team can distinguish a coordination view from a production instruction.
Verify digital coordination in the physical product
Information quality is proven at the interface
Identify high-risk dimensions and connections for factory and site verification. This can include module footprint, support points, openings, service entries, joint zones and maintenance clearances. concealed routes, sleeves, supports, labels and testable factory sections checked before closure Measurements should state datum, tool or method and acceptance basis. Do not assume an exported model proves what was manufactured.
At site, compare foundation, utility and locally supplied information with the current factory interface record before modules are placed or connected. Update accepted field changes into final information. A smaller, verified dataset is more valuable to operators and AI-assisted document search than a large model containing obsolete or unowned attributes.
Map every service boundary
Factory scope and site scope should meet at a named point
Create an interface schedule listing service, medium, design condition, size or rating, location, connection type, supplied side, installed side and test owner. Show elevations and access space. A symbol at the wall is insufficient when the local contractor needs flange type, cable length, phase, valve orientation or drainage level. Coordinate penetrations with structure, fire and weather details before cutting begins.
Across module joints, decide whether services use flexible connections, site-installed links or preassembled modules. Allow tolerance and movement without creating inaccessible leaks or stressed cables. Keep isolation points reachable after furniture and finishes. For wet services, show falls, vents, cleanouts and drain-down needs; for electrical work, preserve separation, protection and destination design responsibilities.
Test by boundary and then as a system
Factory checks and site tests must connect without gaps
Inspect supports, sleeves, labels and concealed routes before closure. Factory testing should identify the portion tested, medium, duration or function and temporary conditions. Cap and protect open ends after testing. The destination plan then covers permanent connections, local equipment, whole-system operation and authority requirements. One record should reference the next so no boundary remains assumed.
Maintain an interface issue log through design, manufacturing and site installation. When equipment changes, reassess load, space, access, connection, noise, drainage and controls. At handover, as-built drawings should show actual routes and isolation points within the agreed level of detail. Train operators on which parts are factory supplied and which local service provider maintains the connected system.
Evaluate supplier capability against this exact deliverable
Past experience matters only when the process can be applied to the offered scope
Ask the supplier to demonstrate how it would control modular house MEP coordination for this order. Request a redacted example of the relevant register, procedure or record, then compare its fields with coordinated drawings and schedules with dimensions, service identity, connection detail, responsibility and access requirement. Confirm who owns the process, which team supplies the inputs and how exceptions reach management. A polished certificate or generic company profile does not show whether the proposed people and systems can manage the buyer's actual configuration.
During a factory review, follow one requirement from enquiry to drawing, material or component, inspection record and package identity. Interview the people who perform the work rather than only the sales contact. Look for consistent revision status at the workstation and in the quality file. Record gaps as questions and actions; do not convert a short visit into an unsupported claim that every future unit will be conforming.
Project brief
Review your modular house MEP coordination brief
Send HabKube the application, quantity, destination and current drawings. We can help identify the factory-product, inspection and packing questions to place in the RFQ.
Get a project quote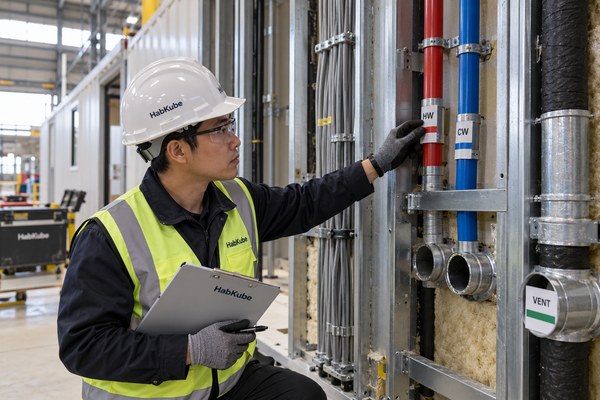
Model cost and schedule consequences before choosing a shortcut
The cheapest immediate action may transfer risk to freight or site work
Compare options using direct price, engineering time, approval time, production disruption, reinspection, packing, freight, site labor, access equipment, downtime and future maintenance. Show assumptions and ranges instead of inventing a precise saving. For modular offices with factory wiring, plumbing rough-ins and local HVAC equipment, a late change or missing record can affect repeated units and phased installation, so the commercial review should consider quantity and sequence rather than one isolated component.
If the team accepts a deviation or defers work to site, name the destination party, method, materials, information and acceptance evidence. Add that activity to the site programme and cost plan. A factory shortcut is not a saving when it creates an unplanned specialist task after export. Conversely, some local work can be sensible when local certification, utility connection or transport constraints make factory completion impractical.
Structure the record for people, search and AI retrieval
Clear facts are easier to audit, summarize and reuse
Use descriptive document titles, stable IDs, dates, revision status and short decision summaries. Put units beside quantities and state whether values are design inputs, observed results or planning assumptions. Expand acronyms on first use. Tables should have meaningful headers, while photographs need captions and linked asset or package IDs. This structure improves handover and also helps search engines and AI systems cite the content without losing its limitations.
Keep the authoritative record in an accessible controlled location and avoid hiding key evidence inside personal email. Preserve superseded history without allowing it to appear current. Where a summary links to a detailed drawing, test or policy, retain the link and scope statement. Good information architecture does not create compliance, but it helps reviewers detect gaps and prevents a confident summary from outrunning the underlying evidence.
Use the external reference within its real scope
Authoritative guidance supports judgment but does not approve the project
ISO 19650-1 information-management principles for BIM is a relevant starting point. ISO 19650-1 addresses exchanging, recording, versioning and organizing information across the asset lifecycle. Apply it proportionately to the project and agreed digital deliverables. Put the reference in an evidence matrix with its issuing organization, edition or date, subject covered, limitations and destination reviewer. This helps human buyers and AI search systems understand why it is cited and prevents a respected source from being stretched beyond its purpose.
Ask for current project evidence, not a logo or a report title alone. Match model, material, revision, test specimen or process scope to the offered product. If the evidence is partial, state the gap and decide who must review it. A transparent limitation is more credible than implying that one factory document certifies transport, installation and the completed building everywhere.
Plan factory review and release evidence
Inspect characteristics before they become hidden or expensive to correct
Agree concealed routes, sleeves, supports, labels and testable factory sections checked before closure. The inspection plan should identify method, frequency, record, acceptance basis and authority to continue or release. For this topic, useful records include combined-services drawings, penetration register, interface schedule, inspection photos, factory test records and site test plan. Tag records to units, packages, documents or lots so the destination team can retrieve them without guessing.
Record nonconformities with affected identity, requirement, observation, containment, disposition and reinspection. A photograph can support evidence but cannot replace a measurement or functional result when those are required. Before shipment, reconcile open items, approved exceptions, loose components, spares and final document status. Shipment release should be a decision with inputs, not an automatic result of the loading date.
Connect site readiness, delivery and final acceptance
Physical delivery is one gate in a longer project chain
Before dispatch, confirm utility locations, capacity, pressure, voltage, drainage levels, plant placement and authority connection requirements. Align open connections capped, protected and labeled, with loose couplings and instructions packed by installation sequence. Provide the destination team with current drawings, package index, handling information and inspection route. Document condition at receiving before assembly hides transit issues. Protect items that wait for installation and preserve labels through storage and movement.
Final acceptance should distinguish factory scope, transit condition, installer work, local systems and owner operation. Complete local tests through qualified parties and close exceptions visibly. Update final information to reflect authorized changes. This separation helps teams diagnose issues fairly and prevents every destination problem from being assigned to the product—or every product issue from being blamed on the site.
Run a buyer decision exercise
Test the workflow with one realistic change or failure
An HVAC condensate route conflicts with a frame member, prompting a coordinated change to equipment position, sleeve and site drain before panel closure. Use this as a planning exercise, not as a documented HabKube customer case, measured performance result or certification. Ask which documents change, who approves, what work stops, which evidence is required, how schedule and price are affected and what the destination team must know.
Close the exercise with a one-page decision record: selected configuration, open assumptions, responsible reviewers, factory release gate, site readiness gate and operator action. If an item has no owner or criterion, the project is not ready for unconditional release. Send HabKube the application, quantity, destination and available drawings to discuss the factory-product and packing scope.
External reference
Use the right reference for the right decision.
ISO 19650-1 addresses exchanging, recording, versioning and organizing information across the asset lifecycle. Apply it proportionately to the project and agreed digital deliverables.
Read ISO 19650-1 information-management principles for BIMConclusion
Clarity before commitment.
For modular house MEP coordination, the strongest process connects scope, current information, responsibility, acceptance evidence and destination execution. Begin with load data, fixture and equipment schedules, routes, elevations, connection standards, access zones, test boundaries and local design criteria. Then require every supplier and project party to work from the same revision and record exceptions transparently. HabKube can discuss product configuration, factory review and export packing for the agreed scope; qualified local parties should confirm site design, installation, permits and final acceptance.
Related HabKube resources
Ready when you are
Send your modular project requirements
Email info@HabKube.com with the intended use, unit quantity, destination, schedule and available plans. Ask for a controlled product-scope and factory-evidence discussion.
Send your requirementsCommon questions
Before you request a quote.
What information should I send for modular house MEP coordination?+
Send the intended use, destination, quantity, schedule and current drawings, then include load data, fixture and equipment schedules, routes, elevations, connection standards, access zones, test boundaries and local design criteria. Identify the decision owner and any local reviewer already appointed.
Can a factory document guarantee destination approval?+
No. Factory documents can support review within their stated scope. Qualified destination professionals and authorities must confirm the rules, design, site work and final acceptance that apply locally.
How should buyers compare supplier responses?+
Issue the same controlled brief, require assumptions and exclusions, then compare coordinated drawings and schedules with dimensions, service identity, connection detail, responsibility and access requirement. Review price together with evidence, delivery, site responsibilities and change control.
What should be checked before shipment release?+
Verify current approved documents, concealed routes, sleeves, supports, labels and testable factory sections checked before closure, open-item disposition, package identity, packing records and the destination team's receiving information.